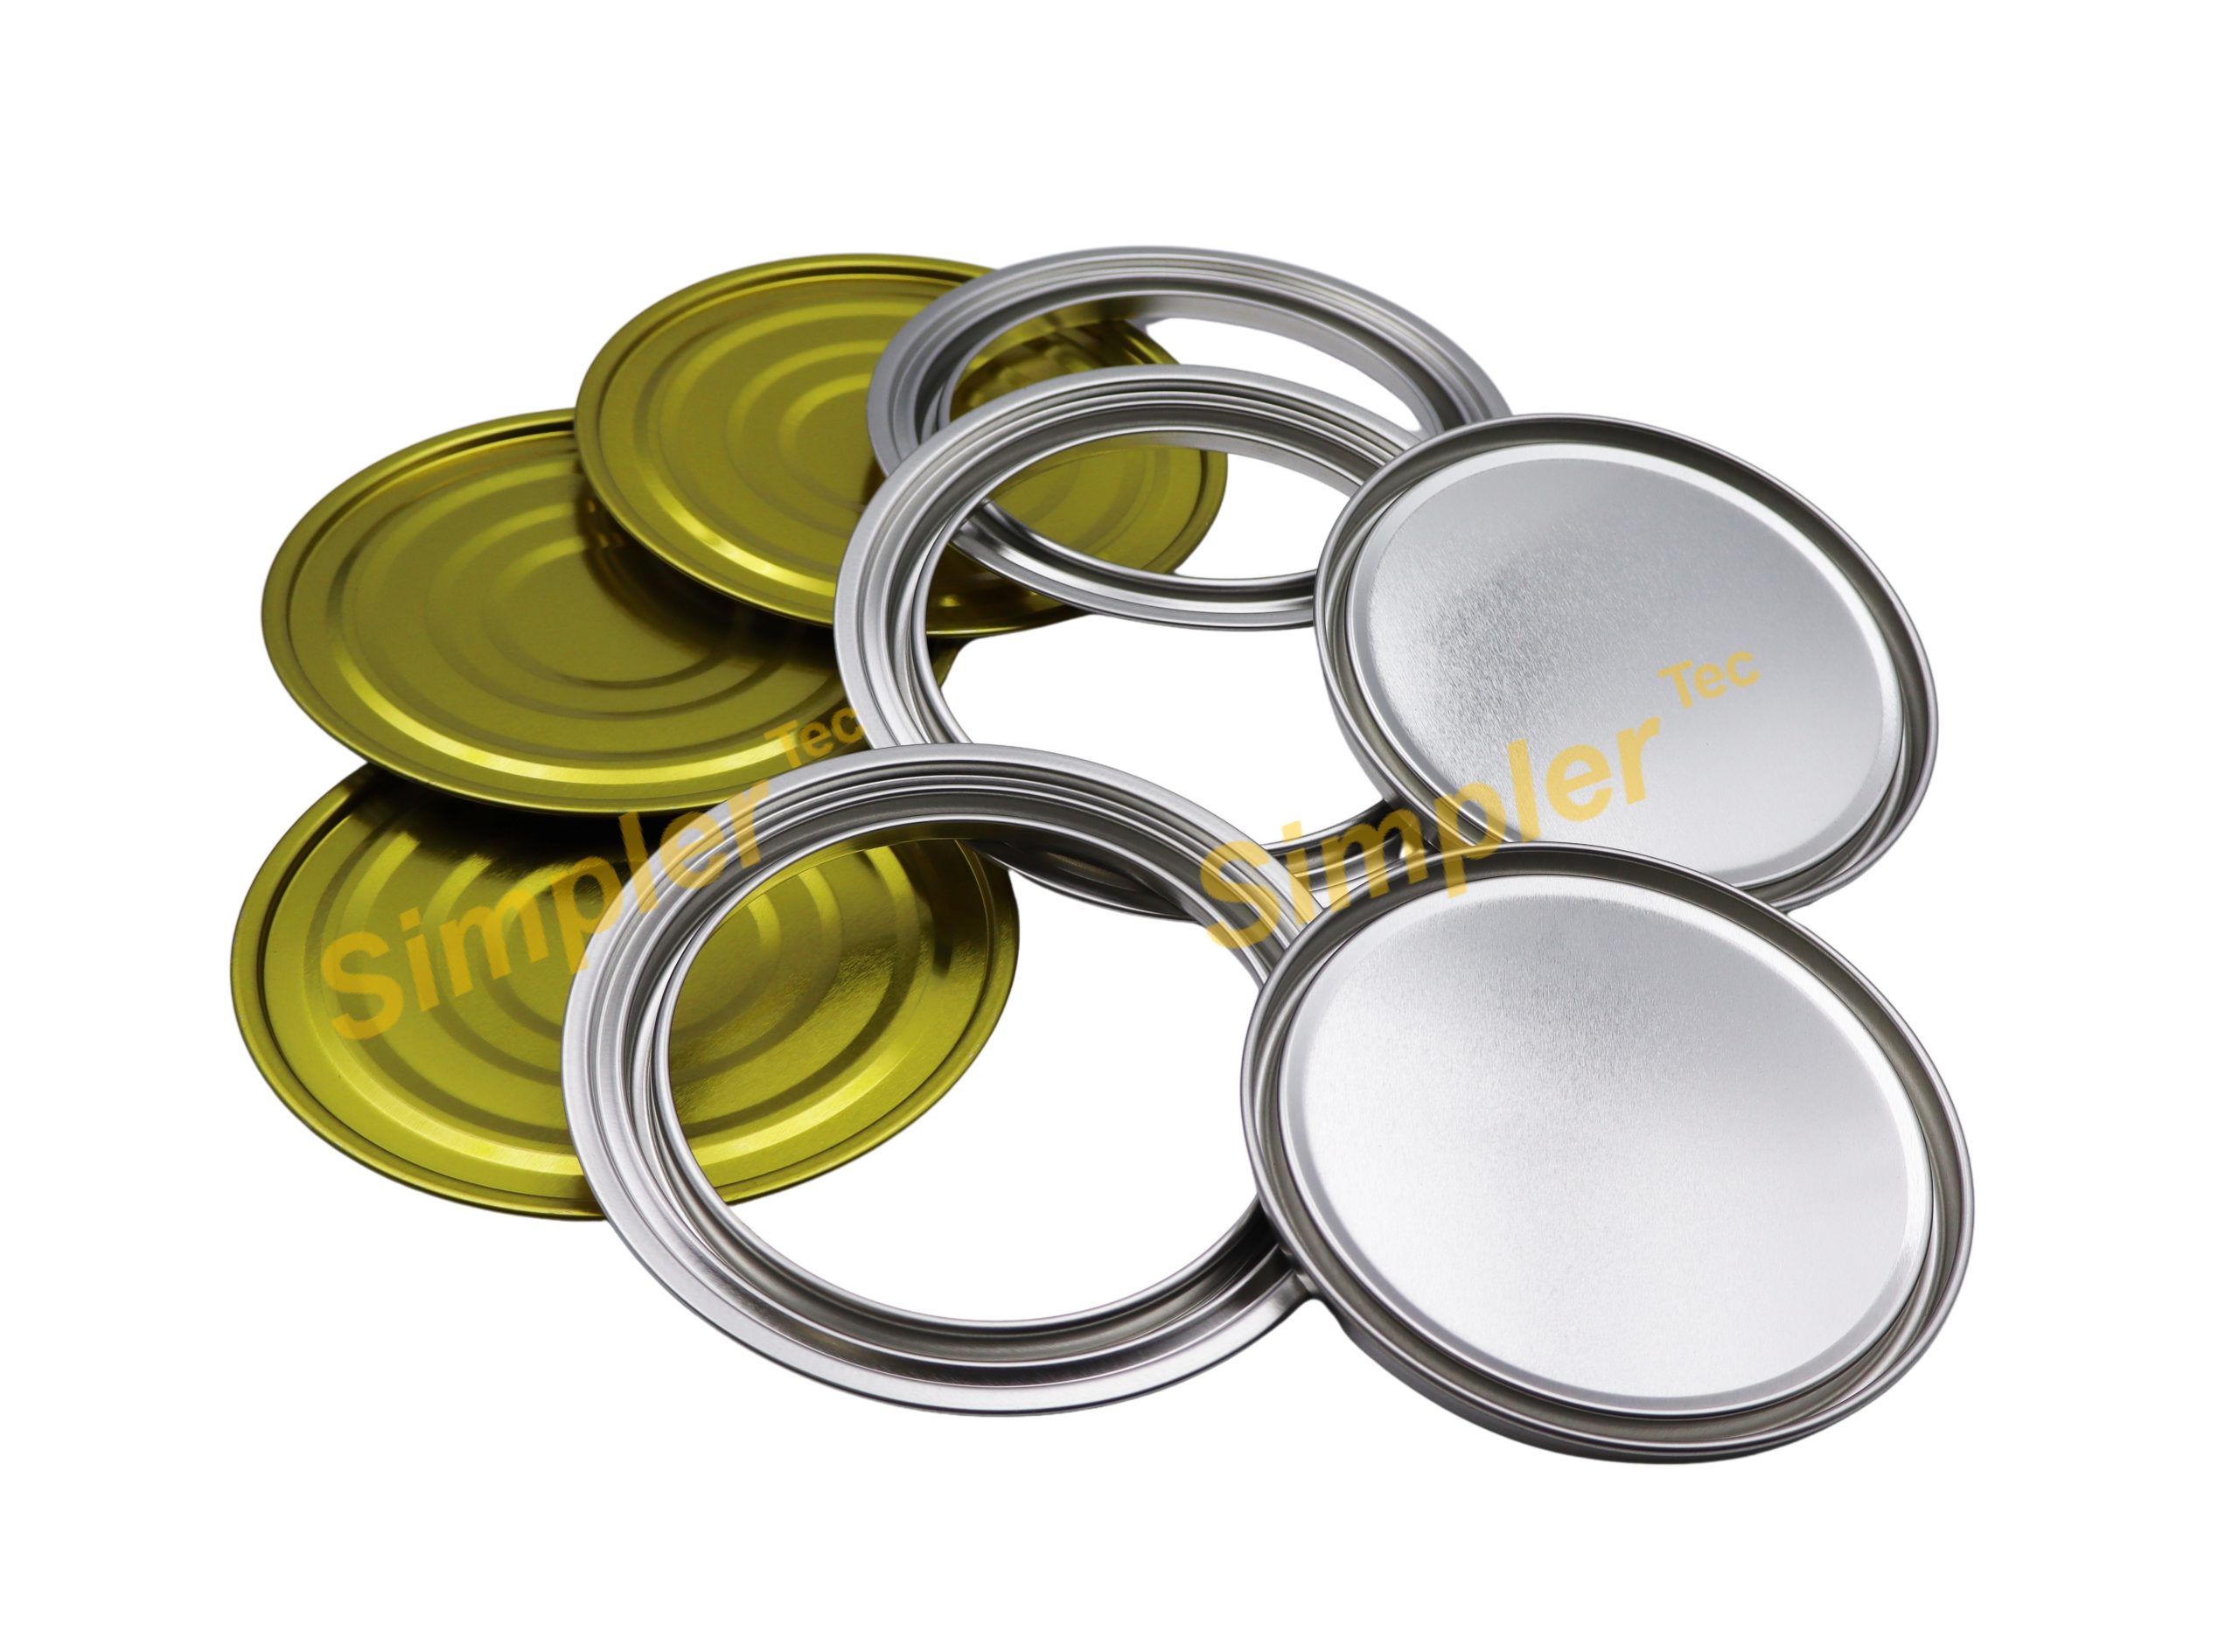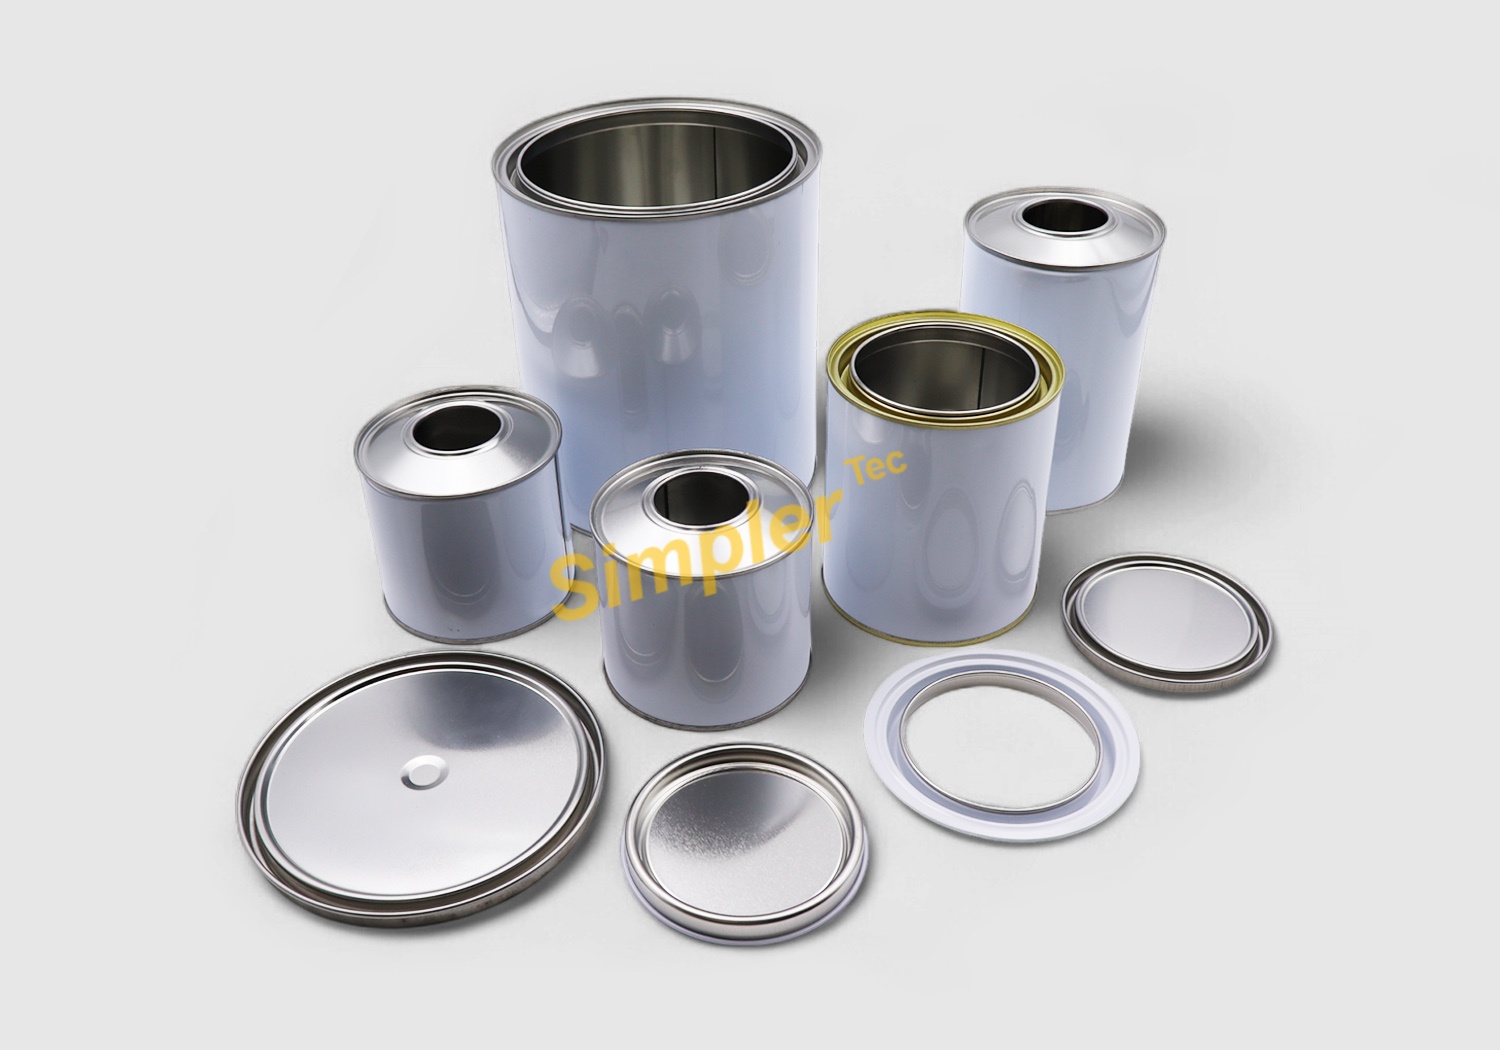
1. Metal Packaging in the Chemical Industry
(1) Protective Properties
- Corrosion Resistance: Metal cans (such as steel or aluminum cans) treated with special coatings can resist corrosion from chemicals such as acids, alkali, and solvents, ensuring the stability of the contents.
- Sealing Performance: Metal packaging offers excellent sealing properties, preventing leakage or evaporation of chemicals, thus ensuring safe transportation and storage.
(2) Safety
- Explosion-Proof Design: Metal cans can withstand high pressures, making them suitable for packaging flammable, explosive, or volatile chemicals.
- Anti-Counterfeiting: Metal packaging can incorporate laser engraving or special markings to prevent counterfeit products from entering the market.
(3) Environmental Friendliness
- Metal packaging is recyclable, reducing the environmental impact of the chemical industry.
- The durability of metal cans minimizes packaging waste, aligning with the green chemistry trend.
(4) Applications
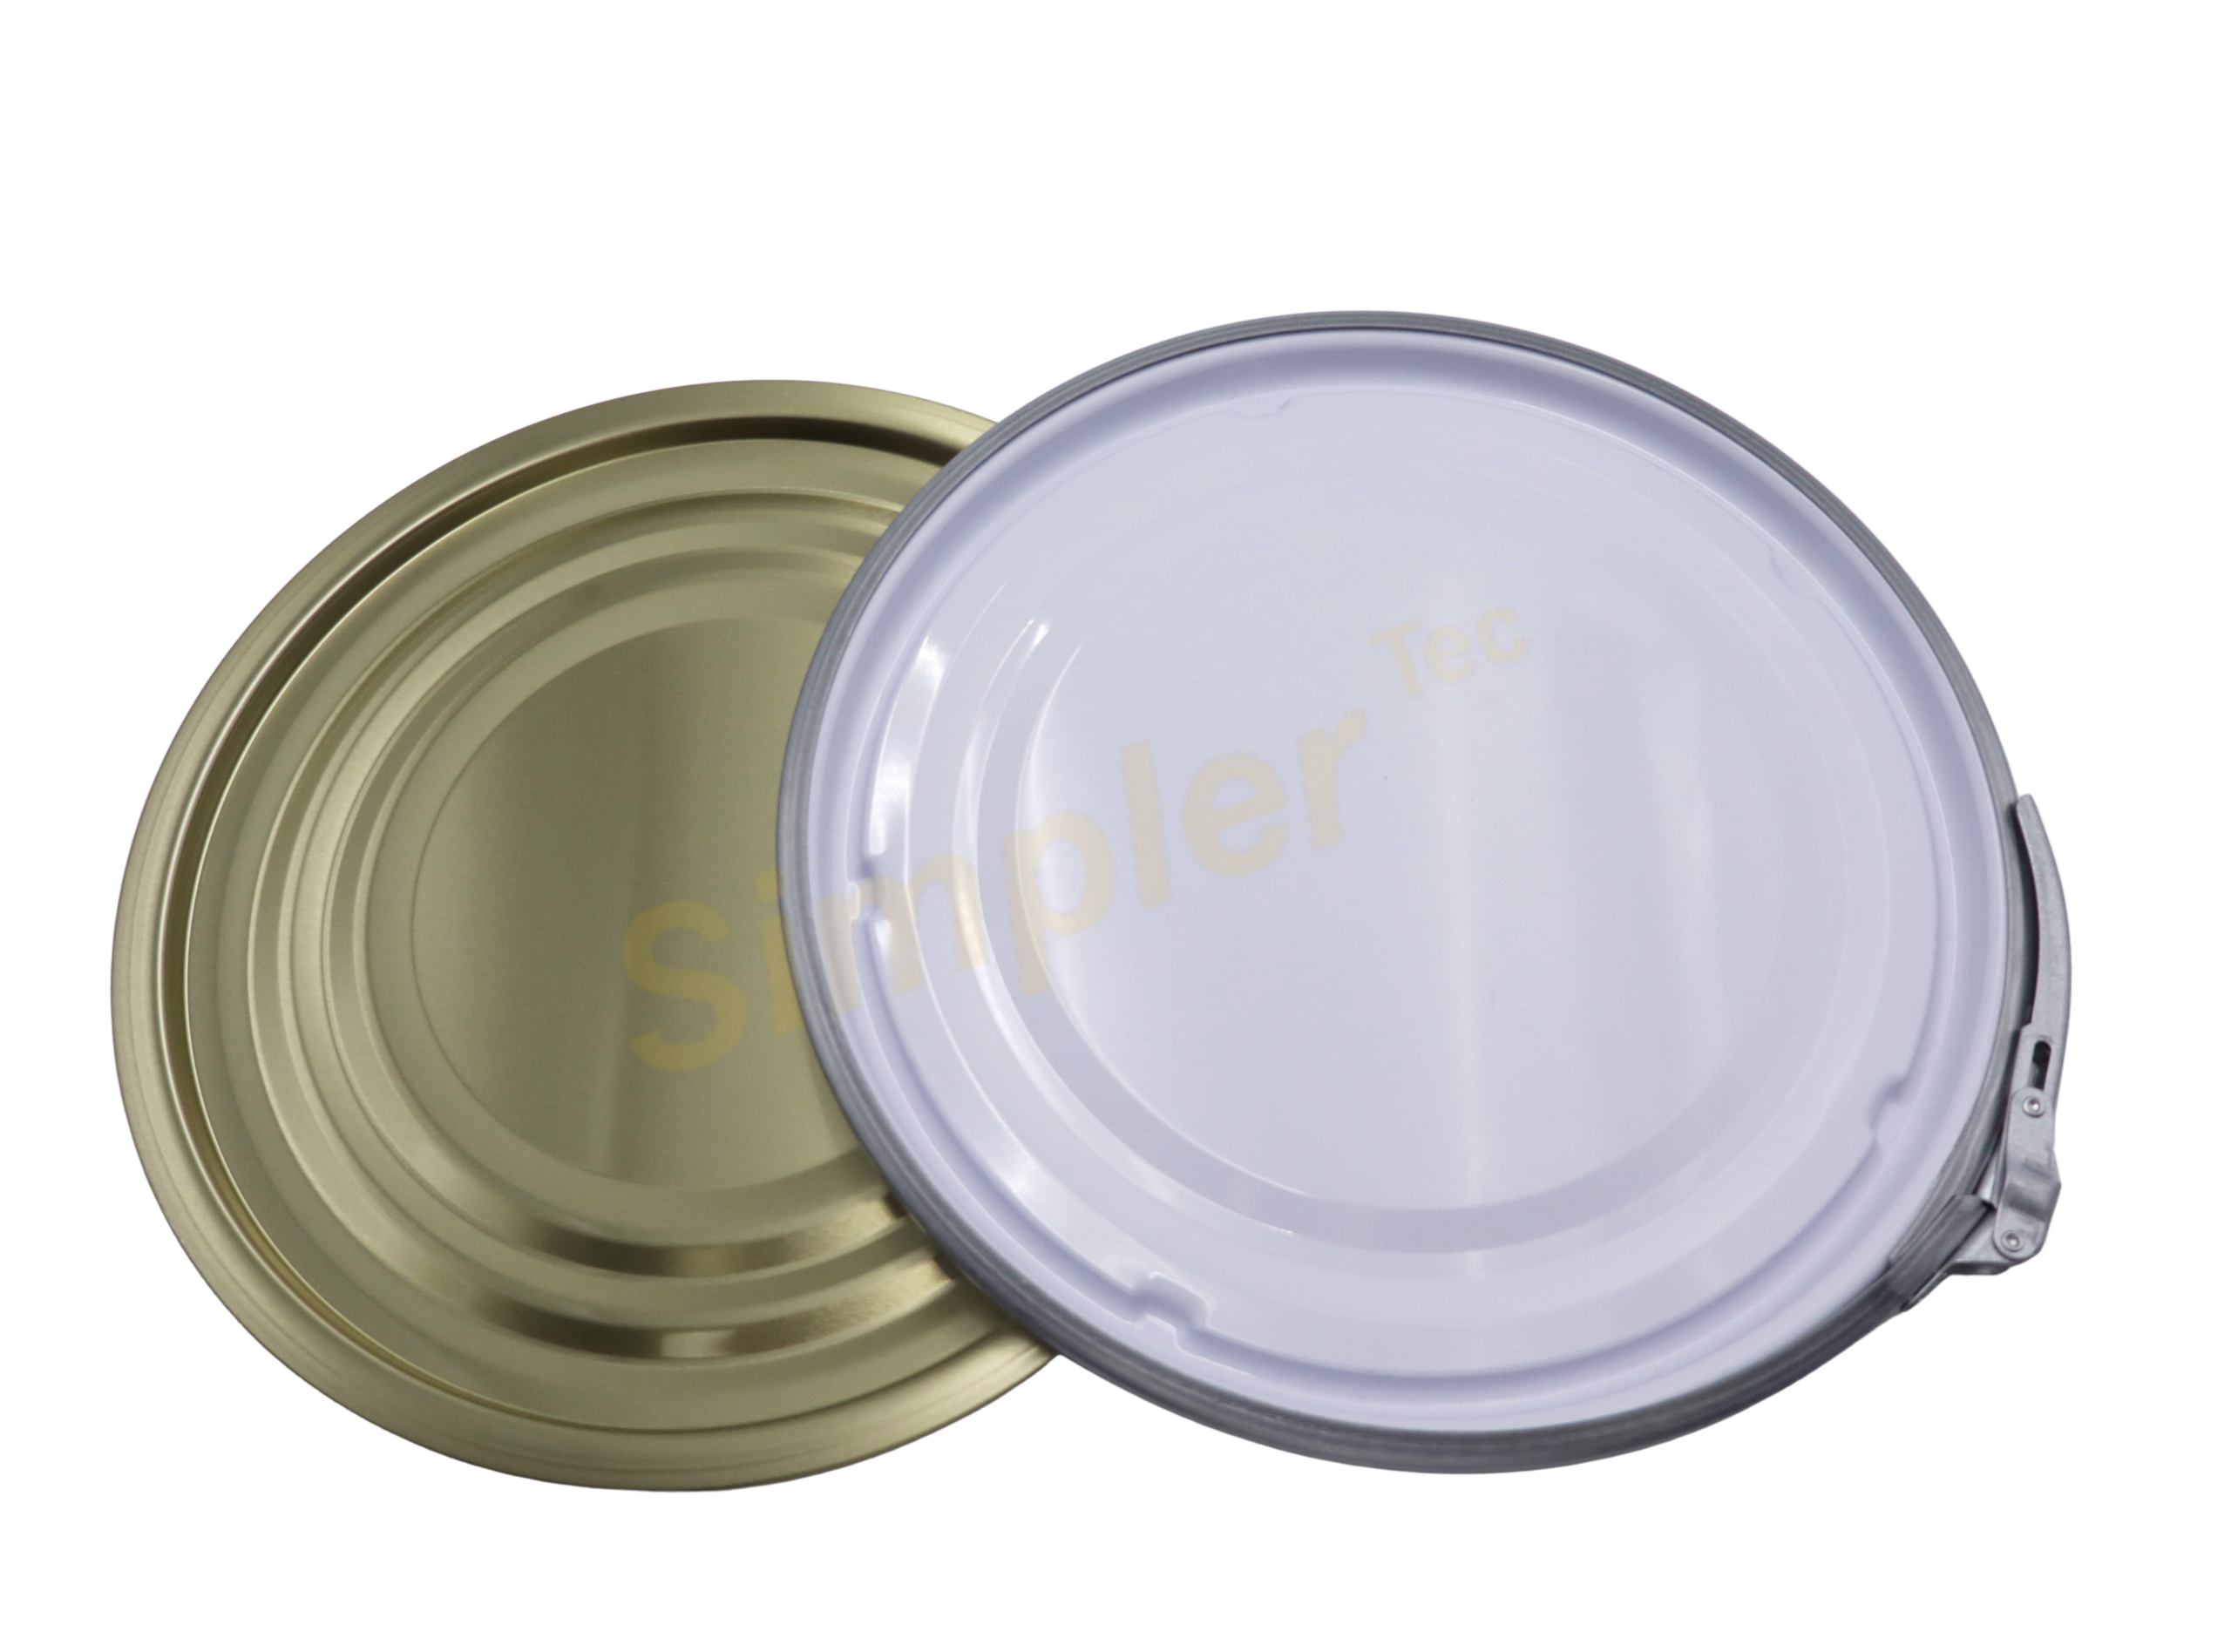
- Packaging for liquid chemicals such as paints, coatings, adhesives, and cleaners.
- Sealing and storage of powder or granular chemicals like dyes and catalysts.

2. Metal Packaging in the Food & Beverage Industry
(1) Freshness and Shelf Life
- Barrier Properties: Metal cans completely block light, oxygen, and moisture, extending the shelf life of food and beverages while maintaining freshness and flavor.
- Sterile Packaging: Metal cans can be sterilized through high-temperature processes, making them ideal for packaging products with high hygiene requirements, such as milk, juice, and baby food.
(2) Portability and Convenience
- Metal cans are lightweight and easy to carry, making them ideal for ready-to-drink beverages (e.g., carbonated drinks, energy drinks) and ready-to-eat foods (e.g., canned goods).
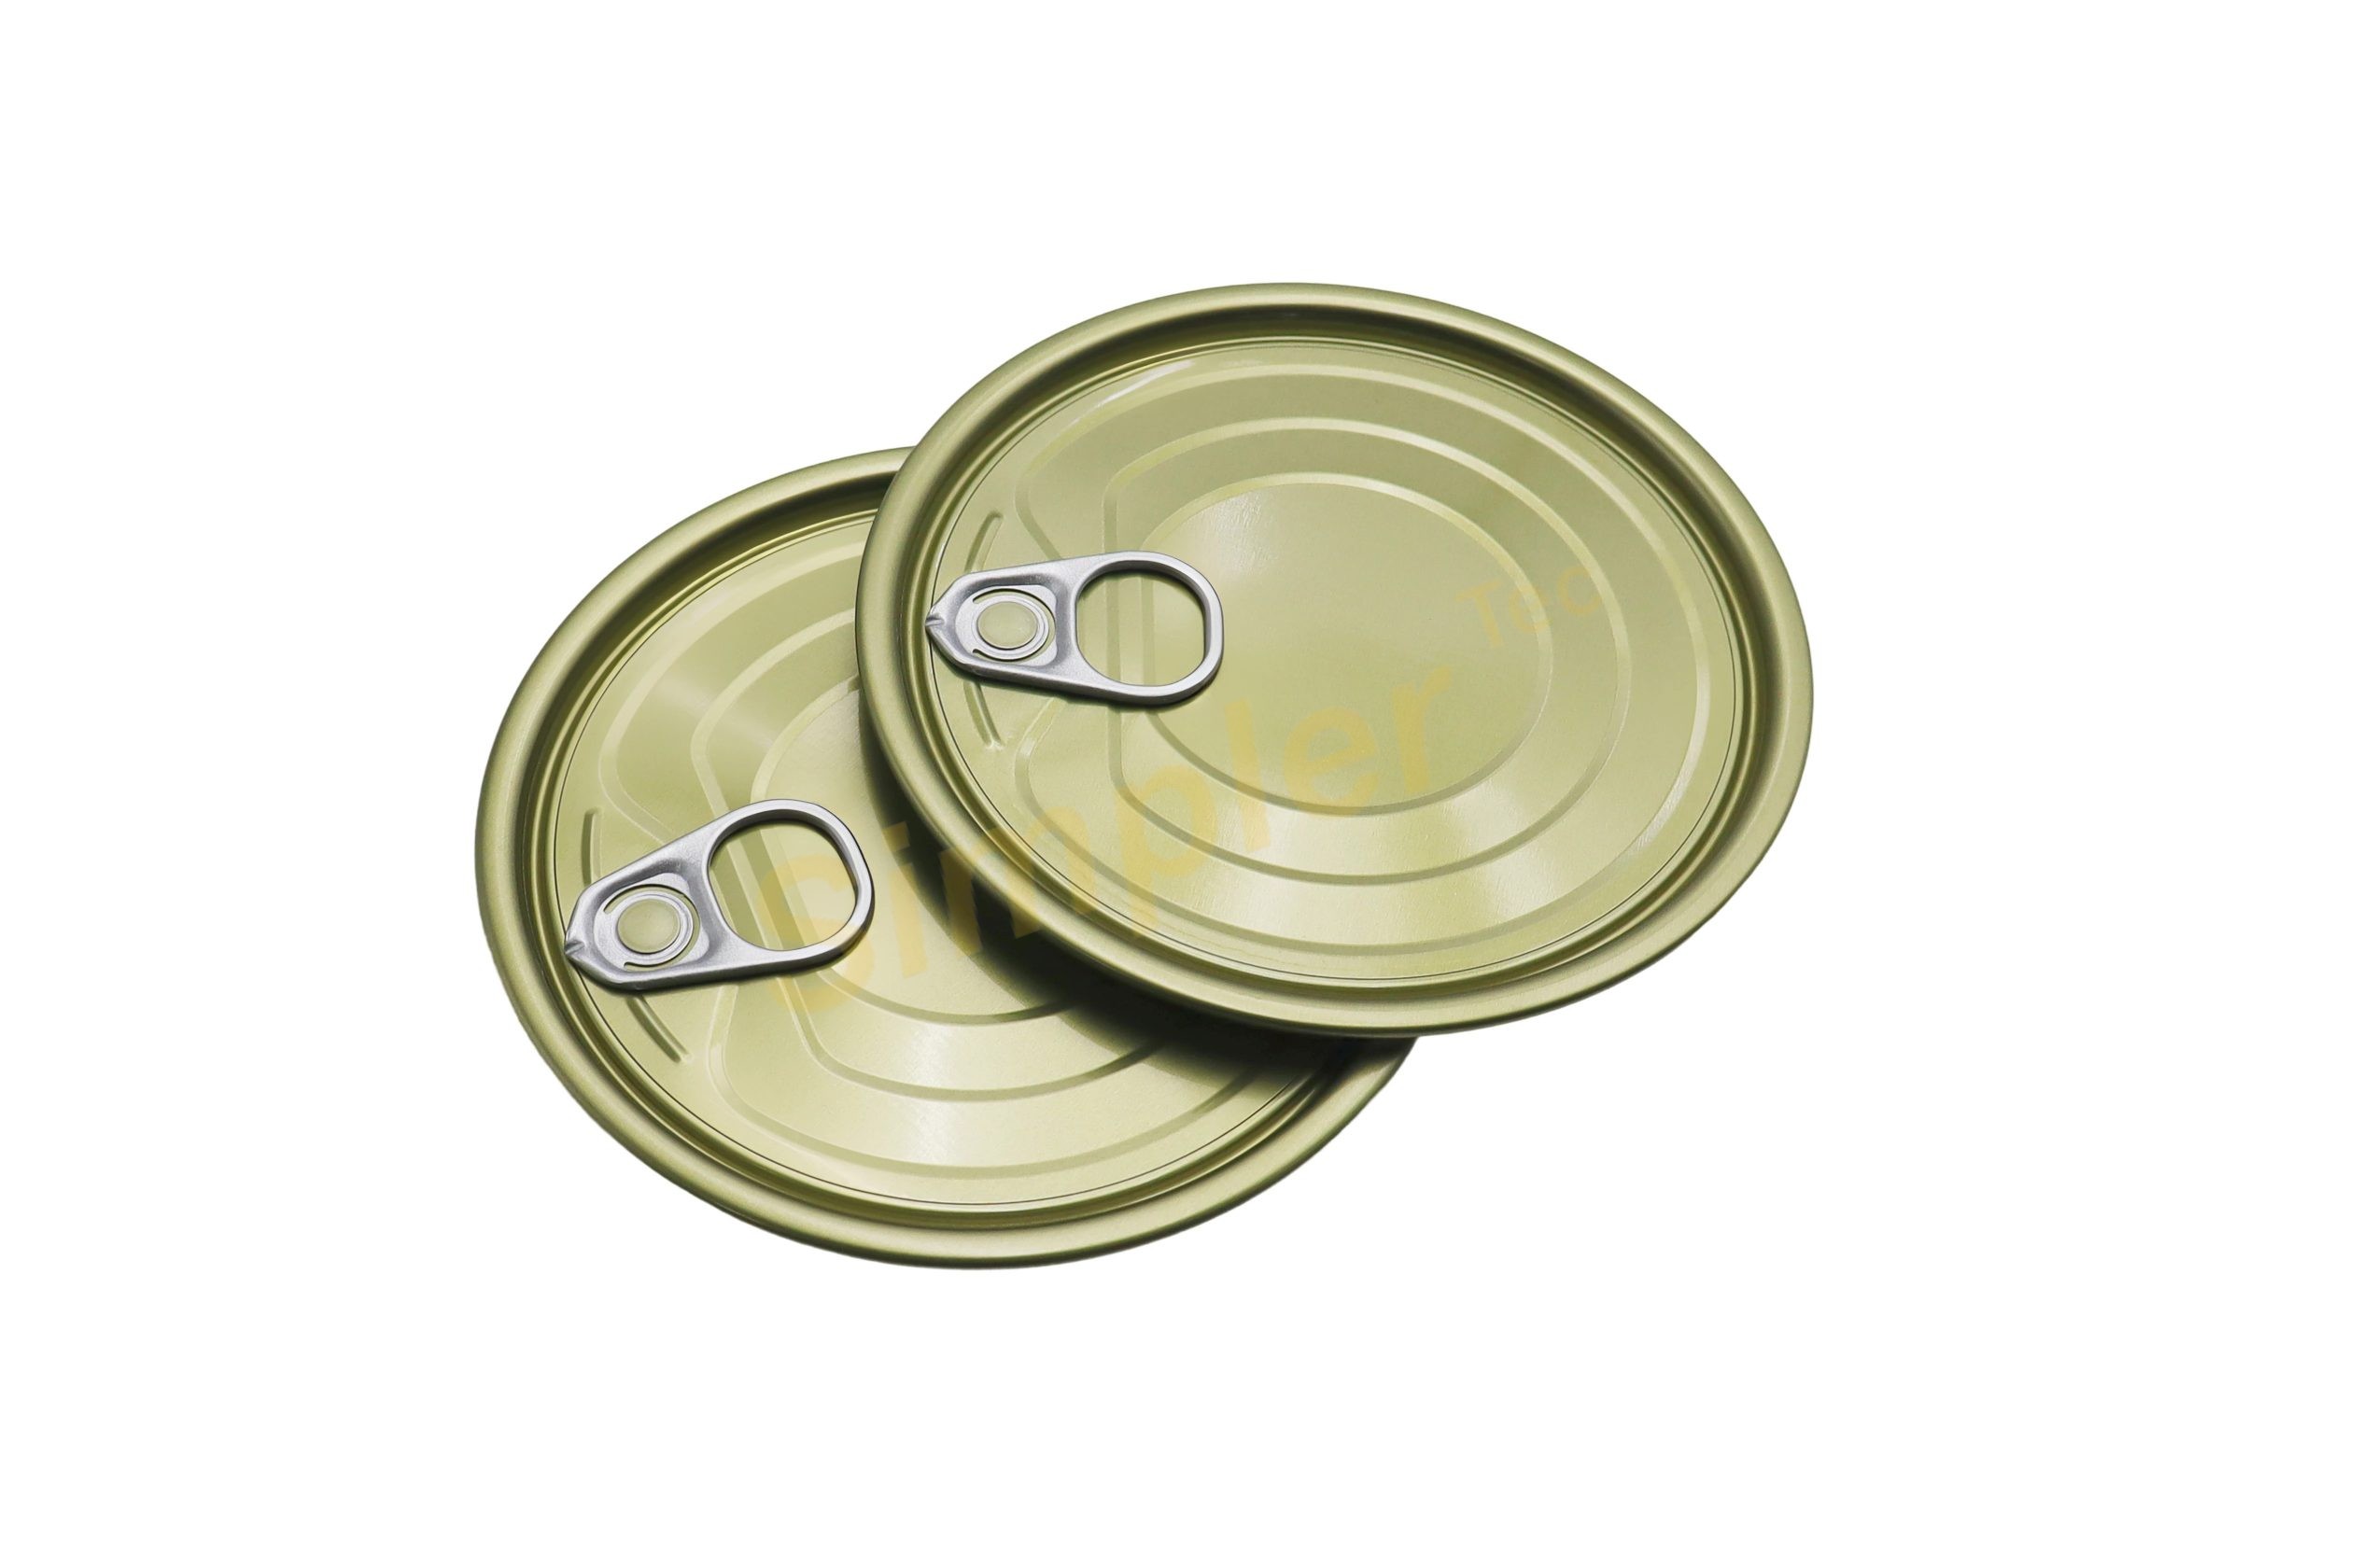
- Easy-to-open designs (such as pull-tab lids) enhance the consumer experience.
(3) Branding and Design
- The surface of metal cans can be precision-printed with vibrant colors and patterns, helping brands build a high-end image.
- Unique can shapes (e.g., slim cans, short cans) and custom designs provide brands with opportunities for differentiated competition.
(4) Environmental Sustainability
- Metal cans have a recycling rate of 70%-90%, supporting the circular economy model.
- Lightweight designs reduce material usage and transportation energy consumption, lowering the carbon footprint.
(5) Applications
- Beverages: Carbonated drinks, beer, energy drinks, tea, coffee, etc.
- Food: Canned food (e.g., fruits, vegetables, meats), milk powder, condiments, snacks, etc.